Home / Products / HS-2230 500°C High-Temperature Inorganic Adhesive
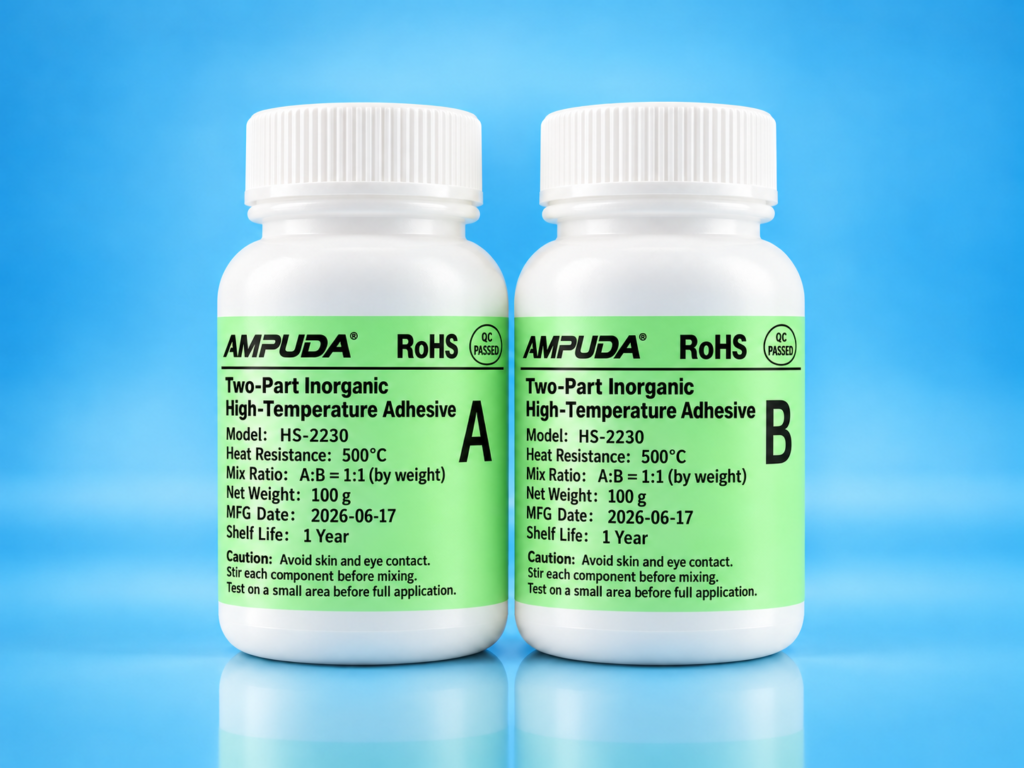
Photo shows A and B bottles labelled 100 g each. Standard supply: 1.6 kg/set or 12 kg/set. The label shows A:B = 1:1; the product specification permits 1:1–2 by weight.
HS-2230 500°C High-Temperature Inorganic Adhesive
Model: HS-2230
Two-part inorganic adhesive for high-temperature bonding, sealing and potting, with continuous service up to 500°C.
- Continuous service temperature up to 500°C
- For heating element seals and sensor potting
- Two-part, heat-cured inorganic adhesive
Packaging: 1.6 kg/set or 12 kg/set
Overview
HS-2230 is a two-part, heat-cured inorganic adhesive for bonding, sealing and potting industrial components operating at temperatures up to 500°C.
Suitable for ceramic joints, heating element end seals, high-temperature sensor potting and threaded or sleeve joints. Validate the adhesive, joint design and cure process on your actual parts before production.
Technical specifications
| Continuous temperature | −40°C to +500°C |
|---|---|
| Short-term peak | +600°C; validate in your application |
| Mix ratio by weight | A:B = 1:1–2 (1 part A to 1–2 parts B) |
| Potting / filling ratio | A:B = 1:1.7–1.8 by weight |
| Mixed material use period | Use within 4 hours |
| Recommended cure | Room temperature 2 h → 40°C 1.5–2 h → 60–70°C 1–2 h → 110°C 4–6 h; cool with the oven |
| Tensile shear strength | ≥1.0 MPa after 100°C × 2-hour cure |
| Pressure resistance | ≥6.0 MPa after 100°C × 2-hour cure; test method not specified |
| Appearance | A: grey viscous liquid; B: white powder; cured: grey-white hard solid |
| Storage | 5–35°C, RH≤70%; cool, dry and ventilated |
| Shelf life | 12 months, sealed and unopened |
Applications
- Industrial heating element end sealing
- High-temperature sensor potting and resistance wire fixing
- Ceramic and lamp base bonding
- Threaded, sleeve and metal groove joint sealing
- High-temperature air purification equipment components
Application & handling
Clean and dry the surfaces. Mix A:B = 1:1–2 by weight until uniform; for potting or filling use 1:1.7–1.8. Prepare only the amount needed and use within 4 hours. Discard lumpy or hardened mixed material.
Recommended staged cure after application: room temperature for 2 hours → 40°C for 1.5–2 hours → 60–70°C for 1–2 hours → 110°C for 4–6 hours, then cool with the oven. The strength values use a 100°C × 2-hour test cure; validate performance with your production process. Room-temperature cure is very slow and is not recommended. Fully cure before further assembly or testing.
Wipe excess uncured adhesive with a water-dampened cloth. Protect cured parts from humidity and store in sealed moisture-protective bags: moisture absorption can reduce electrical insulation. Request the current SDS for safe handling.
Confirm current grade-specific technical and safety data, and validate performance on your actual parts before production.