Home / Products / HS-2260 500°C High-Temperature Spray Coating
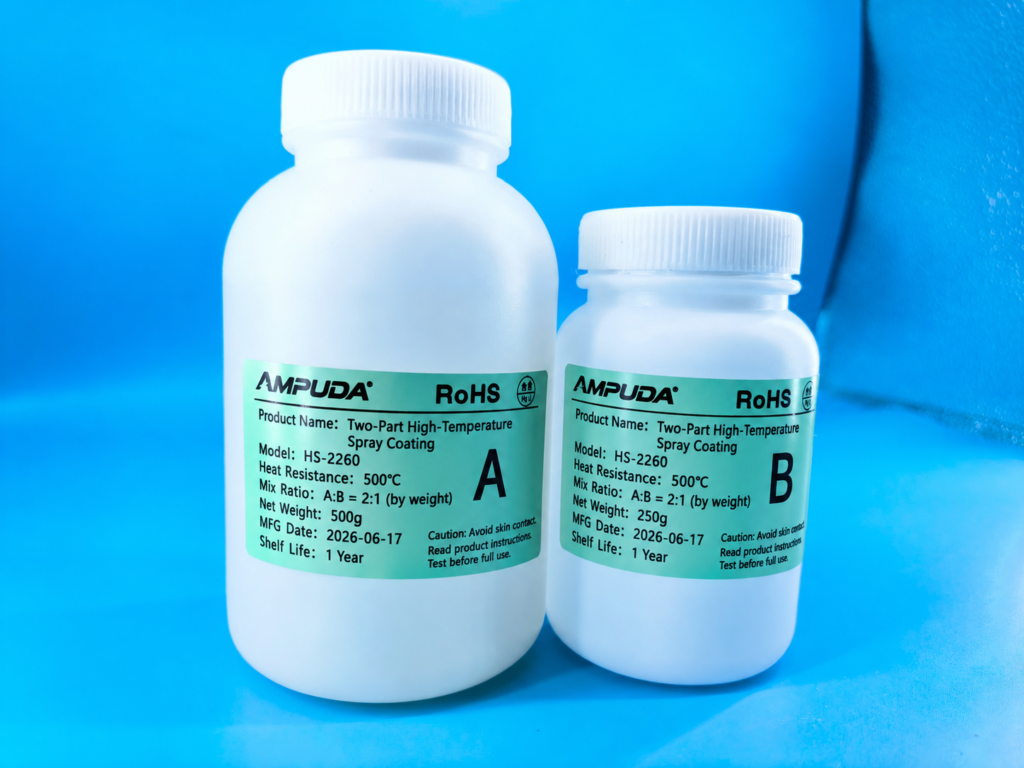
0.75 kg set shown: Part A 500 g + Part B 250 g. Mix ratio A:B = 2:1 by weight.
HS-2260 500°C High-Temperature Spray Coating
Model: HS-2260
Two-part spray or brush coating for metal and ceramic protection, with continuous service up to 500°C.
- Continuous service up to 500°C
- Low viscosity for spray or brush application
- Heat-cured hard film; pencil hardness ≥6H
Packaging: 0.75 kg/set (A: 500 g + B: 250 g) or 3 kg/set
Overview
HS-2260 is a two-part, low-viscosity, heat-cured protective coating for spray or brush application on metal and ceramic surfaces. The supplied specification states continuous service from -55°C to +500°C and a short-term peak of 600°C.
Designed for heating plate protection, moisture protection at electric heating tube ends and high-temperature metal panels. The cured film is colourless to milky white. Confirm substrate adhesion, coating thickness and service conditions before production.
Technical specifications
| Continuous service temperature | -55°C to +500°C |
|---|---|
| Short-term peak temperature | Up to 600°C; validate for the application |
| Mix ratio by weight (A:B) | 2:1 |
| Rest after mixing | 2 hours before application |
| Use limit after mixing | Use within 5 hours, including the 2-hour rest |
| Workable time (source test) | >5 h at 23±2°C and RH≤70% |
| Application method | Spray gun or brush; control single-coat thickness |
| Recommended cure | Preheat workpiece 60°C × 30 min → immediately coat → 180–220°C × 15 min → cool with oven |
| Alternative stated cure | Same preheat and application steps; 200°C × 20 min |
| Mixed density | 1.20–1.40 g/cm³ at 25±0.5°C |
| Mixed pH | 3–6 |
| Cured film pencil hardness | ≥6H |
| Water immersion result | No bubbling, cracking or peeling after full cure and 24 h at 23±2°C |
| Appearance | A: colourless or pale white liquid; B: transparent liquid; cured: colourless to milky-white hard film |
| Storage / shelf life | 5–35°C; 12 months from manufacture in sealed original packaging |
Applications
- Heating plate protective coating
- Moisture protection at electric heating tube ends
- High-temperature metal panel protection
- Spray or brush coating on suitable metal and ceramic substrates
Application & handling
Clean and dry surfaces; remove oil. Roughen metal by sanding or blasting as appropriate. Mix A:B = 2:1 by weight, rest for 2 hours and use within 5 hours from mixing. Discard lumpy, gelled or noticeably thickened material.
Preheat the workpiece to 60°C for 30 minutes, remove and immediately spray or brush. Control single-coat thickness. Cure at 180–220°C for 15 minutes and cool with the oven. The specification also lists 200°C for 20 minutes after the same preparation; validate the selected schedule. Room-temperature curing is not recommended.
Fully cure before machining or testing. Keep bottles tightly sealed against moisture. Wipe uncured excess with a water-dampened cloth. Follow the current SDS for spray ventilation and protective equipment.
Confirm current grade-specific technical and safety data, and validate performance on your actual parts before production.